

Crystalline Solids Pneumatic Conveying: A Material Handling Solution to Overcome Distance Limitations
For industries dealing with crystalline materials, efficient and reliable material handling is crucial. Traditional methods often face limitations when it comes to transporting these materials over long distances or across complex layouts. This is where pneumatic conveying systems, specifically designed for crystalline solids, offer a transformative solution. By leveraging air to transport powders and granules, these systems provide a flexible and effective way to overcome distance barriers and enhance operational efficiency.
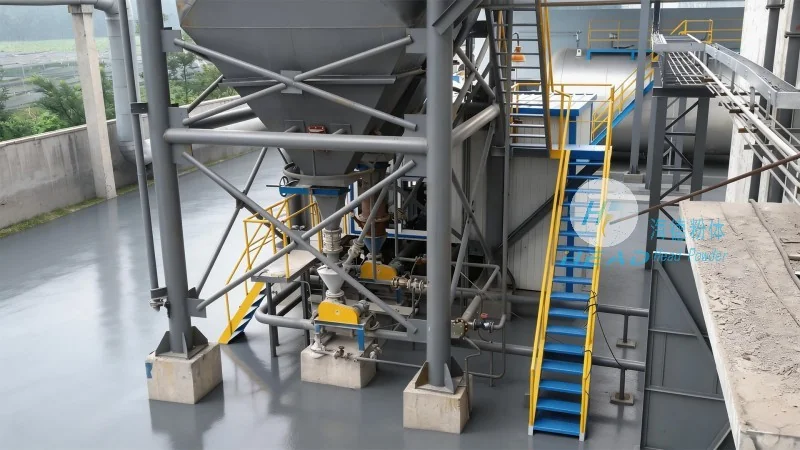
HeadPowder Engineering: Your Expert in Pneumatic Conveying
Shandong HeadPowder Engineering Co., Ltd. is a leading provider of advanced material handling solutions, specializing in the design, manufacturing, and implementation of pneumatic conveying systems tailored for crystalline solids. With years of experience in the industry, HeadPowder has established itself as a trusted partner for businesses seeking to optimize their material transport processes. The company’s commitment to innovation and quality ensures that each system is engineered to meet the unique requirements of its clients, delivering performance that exceeds expectations.
Key Features of Crystalline Solids Pneumatic Conveying Systems
Crystalline solids pneumatic conveying systems are engineered to handle the specific challenges associated with transporting crystalline materials. These systems utilize positive or negative pressure to move materials through a network of pipes, ensuring minimal product degradation and maintaining product integrity. Key features include: high efficiency in long-distance transport, low maintenance requirements, and versatility in handling various crystalline materials. The technology allows for seamless integration into existing production lines, reducing downtime and increasing overall productivity.
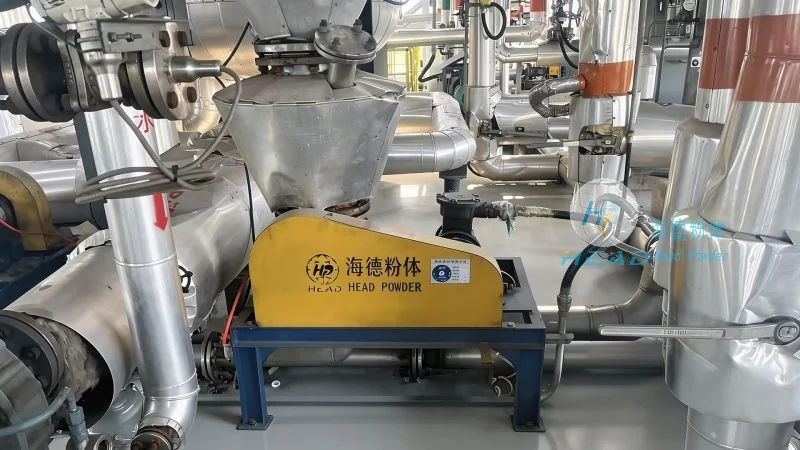
Applications in Diverse Industries
The versatility of crystalline solids pneumatic conveying makes it applicable across a wide range of industries. In pharmaceutical manufacturing, these systems are used to transport active pharmaceutical ingredients (APIs) and excipients with precision, ensuring compliance with stringent quality standards. In chemical processing, they facilitate the handling of various chemicals, including fine powders and granules, while maintaining safety and environmental regulations. Additionally, food and beverage industries benefit from these systems for transporting ingredients like sugar, salt, and other food-grade powders, where hygiene and product purity are paramount.
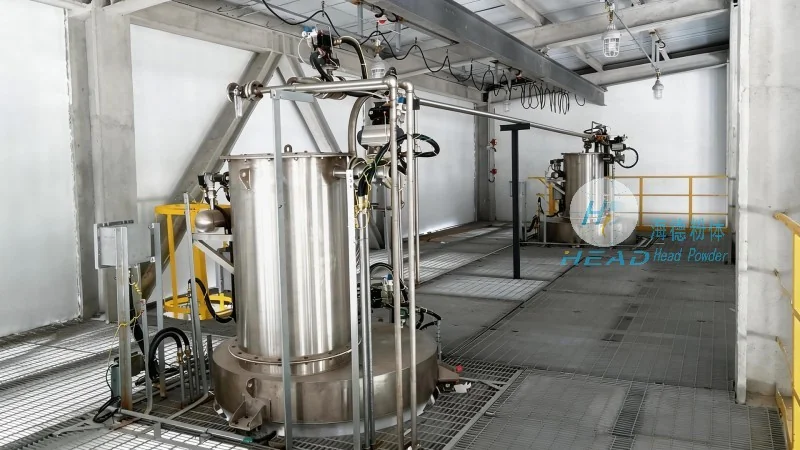
Advantages Over Traditional Conveying Methods
Compared to traditional methods such as belt conveyors or bucket elevators, crystalline solids pneumatic conveying offers several advantages. Firstly, it eliminates the need for multiple transfer points, reducing the risk of material spillage and contamination. Secondly, the system is more compact, allowing for installation in confined spaces without compromising performance. Thirdly, it provides better control over material flow, enabling precise dosing and reducing waste. These benefits collectively contribute to lower operational costs and improved overall efficiency.
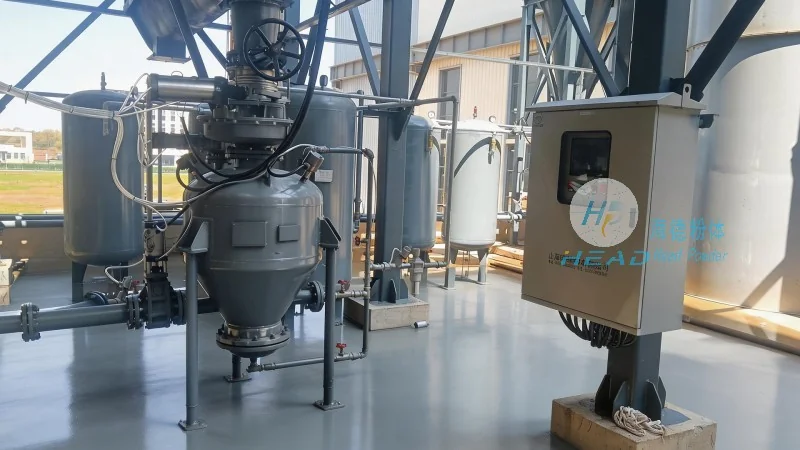
Customization and Integration Services
At Shandong HeadPowder Engineering Co., Ltd., we understand that every industrial application is unique. Therefore, our approach to system design and implementation is highly customized. We work closely with clients to understand their specific needs, from material characteristics to operational constraints, and develop tailored solutions that align with their production goals. Our team of experts provides comprehensive integration services, ensuring that the pneumatic conveying system is seamlessly integrated into the existing infrastructure. This includes installation, commissioning, and ongoing support to guarantee optimal performance and longevity of the system.
Quality Assurance and Compliance
HeadPowder Engineering adheres to the highest standards of quality and compliance in all its operations. Our systems are manufactured using premium materials and advanced technologies, ensuring durability and reliability. We also comply with international standards and regulations, such as those related to food safety and pharmaceutical manufacturing. This commitment to quality ensures that our clients receive systems that not only meet but exceed industry expectations, providing peace of mind and long-term value.