

Working Principle and Features of Fermented Grain Material Conveying System Equipment
Fermented grain material conveying systems are critical components in the production processes of traditional and modern alcoholic beverages. These systems are designed to efficiently transport materials such as fermented grains, which are essential for the fermentation and distillation stages. The proper functioning of these systems directly impacts the quality, consistency, and efficiency of the overall production line. Understanding the working principle and key features of such equipment is vital for manufacturers seeking to optimize their operations and maintain high standards in beverage production.
The Working Principle of Fermented Grain Material Conveying Systems
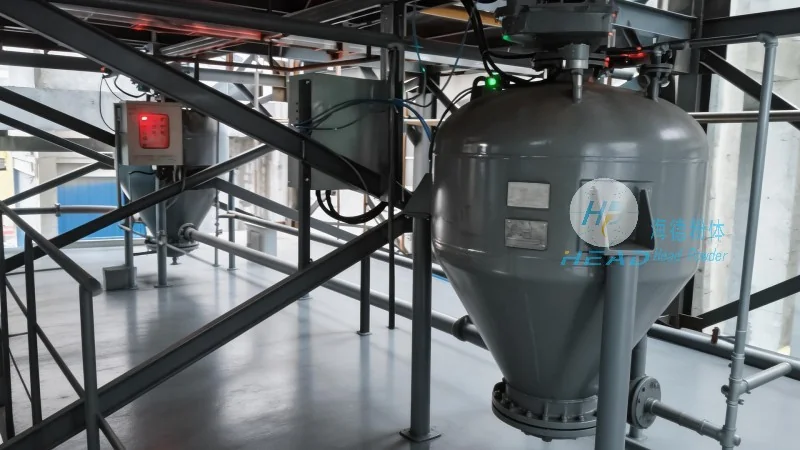
At the core of fermented grain material conveying systems is a combination of mechanical and control technologies tailored to handle the specific characteristics of fermented grains. The process typically begins with the loading of raw materials or intermediate products into the system. Through a series of mechanisms, including conveyor belts, screw conveyors, or pneumatic systems, the materials are transported from one processing stage to another. The working principle involves precise control of speed, direction, and material flow to ensure minimal damage to the fermented grains while maintaining an efficient transfer rate. Advanced systems may incorporate sensors and automation controls to adjust the conveying parameters in real-time, responding to variations in material density, moisture content, or batch size. This dynamic adjustment helps maintain consistent product quality and reduces operational downtime.
Key Features of Fermented Grain Material Conveying Systems
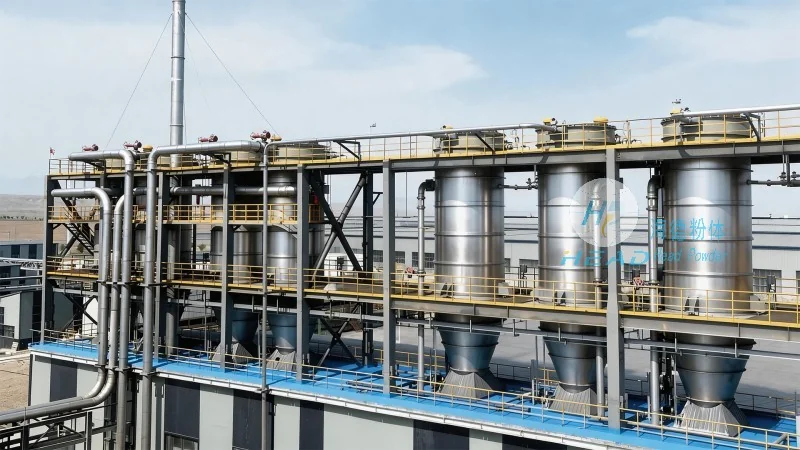
Modern fermented grain material conveying systems are equipped with several advanced features that enhance their performance and reliability. One of the primary features is the use of durable, food-grade materials for construction, ensuring compliance with sanitary standards and preventing contamination of the product. The systems often include adjustable speed controls, allowing operators to customize the conveying rate based on the specific requirements of the production process. Additionally, many models feature easy-to-clean designs with smooth surfaces and removable components, facilitating regular maintenance and sanitation. Another important feature is the integration of monitoring systems, which provide real-time data on material flow, temperature, and system performance. This data can be used for process optimization and predictive maintenance, reducing the risk of equipment failure and increasing overall system uptime. Some advanced systems also incorporate energy-efficient designs, such as variable frequency drives, to minimize power consumption while maintaining optimal conveying performance.
Application Scenarios and Benefits
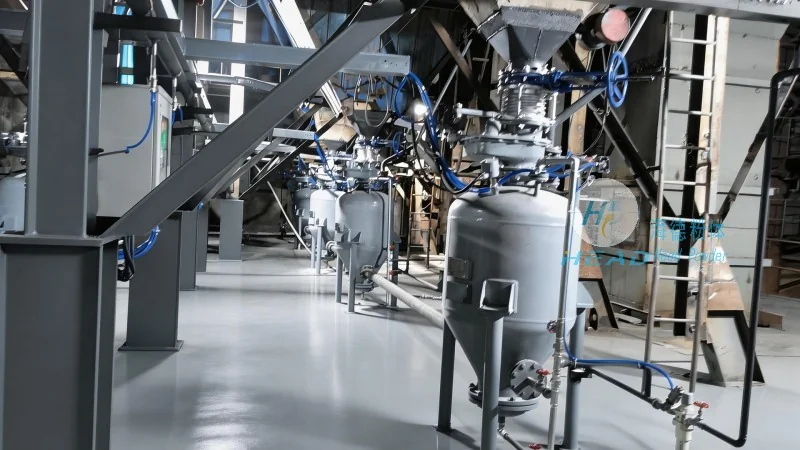
Fermented grain material conveying systems are widely used in various stages of alcoholic beverage production, including the transfer of fermented mash from fermentation tanks to distillation units, the movement of spent grains for further processing or disposal, and the handling of intermediate products during the aging or filtration processes. The benefits of using these systems extend beyond mere material transport. By ensuring a smooth and consistent flow of materials, they help maintain the integrity of the fermented product, which is crucial for achieving the desired flavor, aroma, and alcohol content in the final beverage. Furthermore, efficient conveying systems reduce labor costs and improve overall production throughput, making them a valuable investment for beverage manufacturers. The ability to handle different types of fermented grains, from traditional rice or wheat to modern hybrid blends, also makes these systems versatile and adaptable to diverse production needs.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field of industrial conveying equipment, specializes in the design, development, and production of fermented grain material conveying systems. With a strong commitment to quality and innovation, the company has built a reputation for delivering reliable and efficient solutions tailored to the unique needs of the beverage industry. HeadPowder's products are engineered to meet the highest standards of hygiene and performance, ensuring that they can withstand the demanding conditions of industrial production while maintaining the quality of the fermented materials. The company's team of experienced engineers and technicians works closely with clients to understand their specific requirements and provide customized solutions that enhance operational efficiency and product quality. HeadPowder's facilities, located in Shandong, China, are equipped with advanced manufacturing technologies and stringent quality control processes, ensuring that every product meets the strictest industry standards. By choosing HeadPowder, beverage manufacturers can benefit from years of expertise and a dedicated focus on delivering superior conveying solutions that support their production goals.