

What is a Dust Powder Conveying System Equipment? What are its Design Principles?
The dust powder conveying system equipment is a specialized industrial solution designed to handle and transport powders and dust particles efficiently. This system is crucial in various industries, including chemical, pharmaceutical, food processing, and mining, where the safe and reliable movement of particulate materials is essential. The system typically comprises several key components that work in tandem to ensure smooth and controlled material transport.
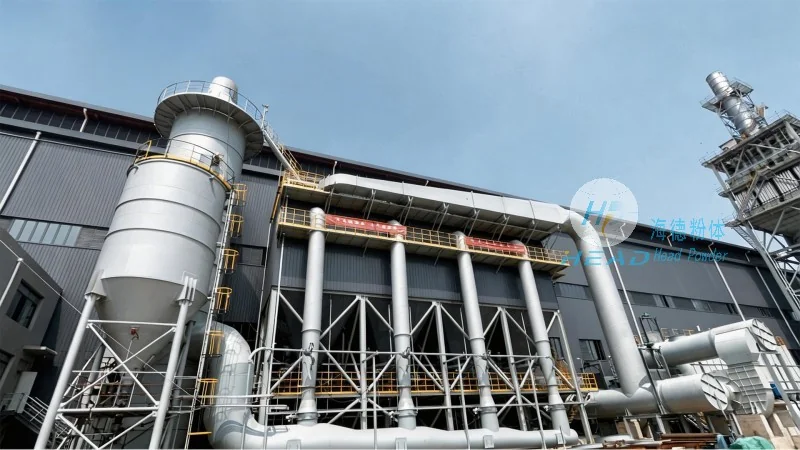
Overview of the HeadPowder Company
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer and supplier of advanced powder handling solutions. With its headquarters located in Shandong, China, the company has established itself as a trusted partner in the industry, offering high-quality equipment and technical expertise. HeadPowder specializes in the design, development, and manufacturing of dust powder conveying systems tailored to meet the specific needs of different industrial applications.
Key Components of the Dust Powder Conveying System
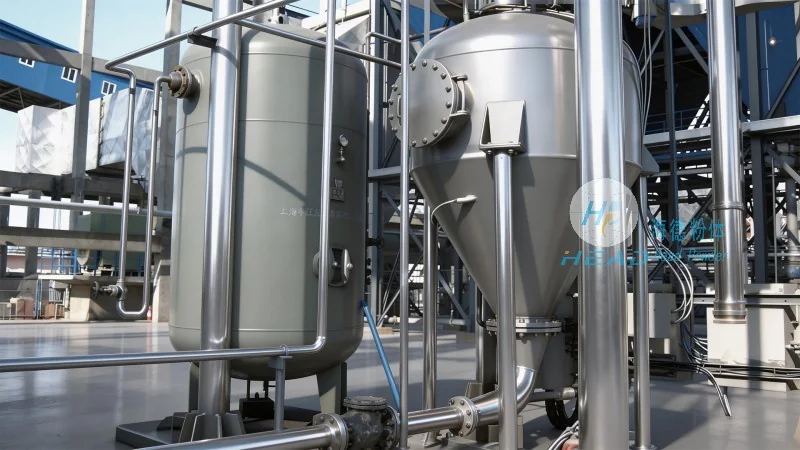
A typical dust powder conveying system consists of several essential components that ensure the efficient and safe transport of powders. These components include:
Conveying hoses or tubing: Flexible or rigid hoses designed to carry the powder material through the system.
Pumps or blowers: Devices that generate the necessary airflow or pressure to move the powder particles.
Dust collectors: Equipment that captures and filters the airborne particles, ensuring compliance with environmental regulations.
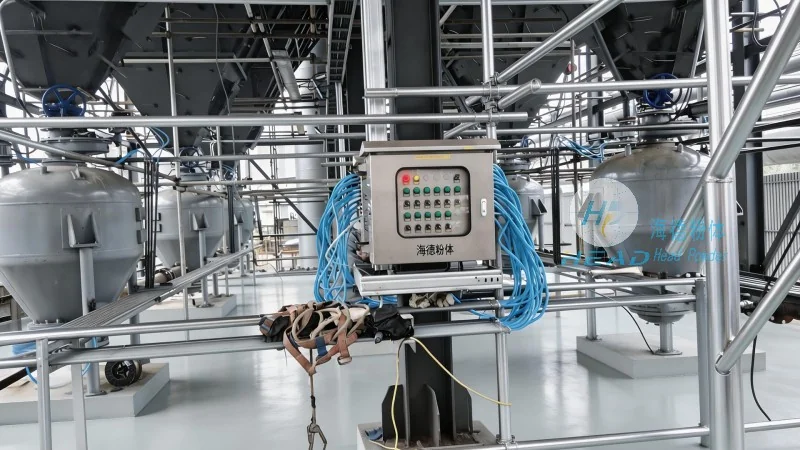
Control systems: Automated systems that monitor and regulate the operation of the conveying process.
Filtration and safety devices: Components that prevent dust emissions and ensure worker safety.
Design Principles and Technical Considerations
The design of a dust powder conveying system follows several fundamental principles to ensure optimal performance. These principles include:
Material compatibility: Ensuring that all components are compatible with the specific powder being transported, considering factors like moisture content, particle size, and chemical properties.
Airflow management: Properly managing the airflow to maintain consistent particle velocity and prevent blockages or clogging.
Pressure and velocity control: Controlling the pressure and velocity of the air to achieve efficient transport without causing excessive wear or damage to the system components.
Energy efficiency: Designing the system to minimize energy consumption while maintaining high transport efficiency.
Safety and environmental compliance: Incorporating features that ensure the system operates safely and meets environmental regulations regarding dust emissions.
Applications and Benefits of the System
The dust powder conveying system is widely used in various industrial applications, offering several benefits over traditional methods of powder transport. Some common applications include:
Pharmaceutical manufacturing: Transporting raw materials and finished products in a sterile and controlled environment.
Food processing: Moving food-grade powders, such as flour or sugar, while maintaining hygiene and safety standards.
Chemical processing: Handling hazardous or reactive powders with precision and safety.
Mining and minerals: Conveying ore and other mineral powders from processing plants to storage or further processing facilities.
The benefits of using a dust powder conveying system include:
Improved efficiency: Faster and more reliable transport of powders compared to manual or traditional methods.
Reduced downtime: Minimized maintenance and operational issues, leading to lower downtime and increased productivity.
Enhanced safety: Reduced exposure to airborne dust and improved safety for workers.
Environmental compliance: Effective dust collection and filtration systems that comply with environmental regulations.
Cost savings: Lower operational costs due to energy efficiency and reduced material waste.
Conclusion
In conclusion, the dust powder conveying system equipment, designed and manufactured by companies like Shandong HeadPowder Engineering Co., Ltd., plays a vital role in modern industrial operations. By adhering to sound design principles and incorporating advanced components, these systems provide efficient, safe, and environmentally friendly solutions for the transport of powders and dust particles. The expertise and quality of equipment offered by HeadPowder ensure that industries can meet their operational needs while maintaining high standards of safety and performance.