

What is an Automatic Powder Handling System? What Are Its Design Principles?
Automatic powder handling systems are sophisticated industrial solutions designed to transport, store, and manage bulk powders efficiently. These systems are integral to various industries, including pharmaceuticals, food processing, chemicals, and manufacturing, where precise and reliable powder movement is critical for operational success. The core function of such systems is to automate the handling of powders, reducing manual labor, minimizing material loss, and enhancing overall process control.
Key Components of an Automatic Powder Handling System
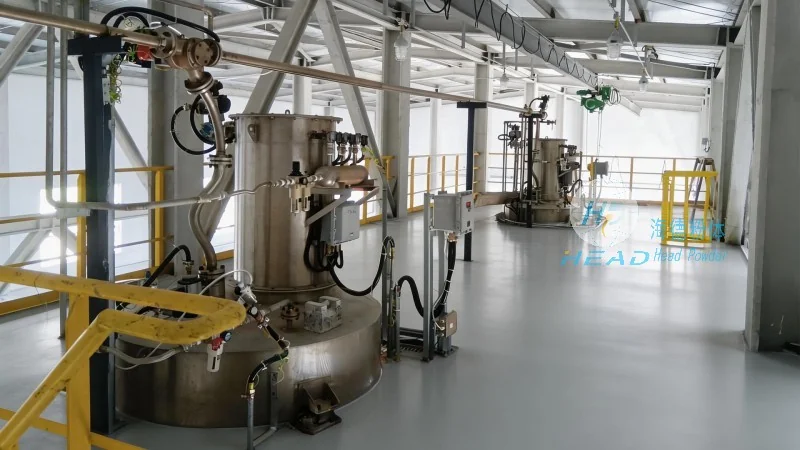
At the heart of an automatic powder handling system are several key components that work in tandem to ensure smooth operation. The primary components include feeders, conveyors, storage silos, and control systems. Feeders, such as rotary or vibratory types, are responsible for metering and feeding powders into the system. Conveyors, including pneumatic or mechanical types, transport the powders from one location to another. Storage silos provide a secure and controlled environment for storing bulk powders, while control systems manage the entire process, ensuring optimal performance and safety.
Design Principles of Automatic Powder Handling Systems
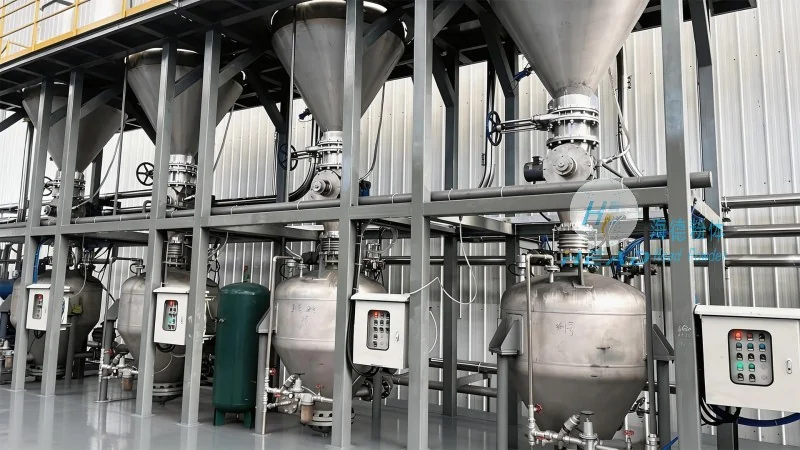
The design principles of automatic powder handling systems are centered on efficiency, safety, and adaptability. Engineers and designers consider several factors when developing these systems, including the physical properties of the powder (e.g., flowability, density, moisture content), the required throughput, and the space constraints of the facility. The design aims to minimize material degradation, prevent contamination, and ensure consistent flow rates. Additionally, the system must be easy to maintain and operate, with clear safety features to protect personnel and equipment.
Applications and Benefits of Automatic Powder Handling Systems
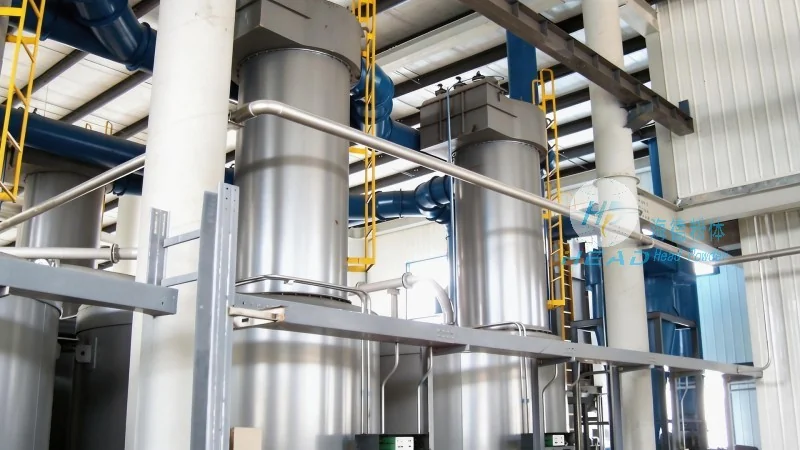
Automatic powder handling systems are widely used across multiple industries due to their versatility and efficiency. In the pharmaceutical industry, these systems ensure the accurate and sterile handling of raw materials, which is crucial for maintaining product quality and regulatory compliance. In the food industry, they help maintain hygiene standards and prevent cross-contamination. In chemical manufacturing, they enable the safe handling of hazardous powders, reducing the risk of accidents. The benefits of these systems include increased productivity, reduced labor costs, improved product quality, and enhanced safety in the workplace.
Customization and Integration with Existing Systems
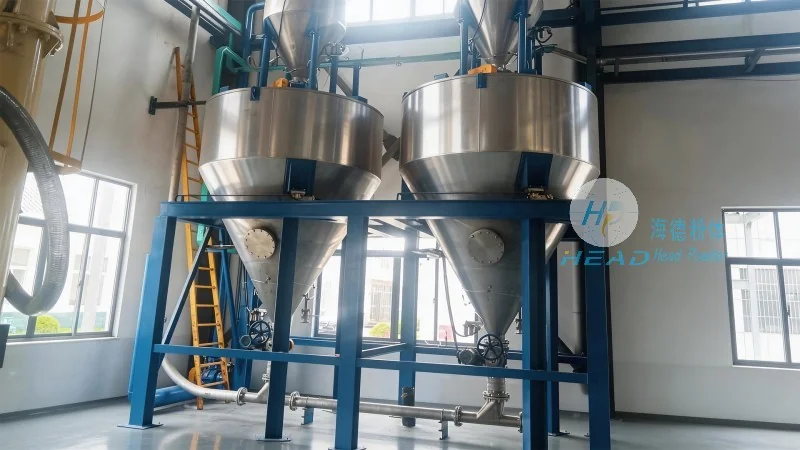
Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, specializes in designing and manufacturing customized automatic powder handling systems tailored to specific client needs. The company understands that each industrial application has unique requirements, and thus, they offer flexible solutions that can be integrated with existing infrastructure. Their expertise lies in creating systems that not only meet but exceed industry standards, ensuring long-term reliability and performance. By working closely with clients, HeadPowder engineers can develop solutions that optimize material flow, reduce downtime, and enhance overall operational efficiency.