

[Efficient Airflow Conveying Systems for Molybdenum Oxide Transport Solutions]
For industrial applications involving the handling of molybdenum oxide, the selection of an appropriate material transport method is critical to operational efficiency and safety. Traditional methods such as mechanical conveyors may face challenges when dealing with fine powders like molybdenum oxide, often leading to issues including dust generation, material degradation, and system blockages. In response to these challenges, modern airflow conveying systems have emerged as a highly effective solution, offering a reliable and efficient means to transport molybdenum oxide while minimizing operational risks.
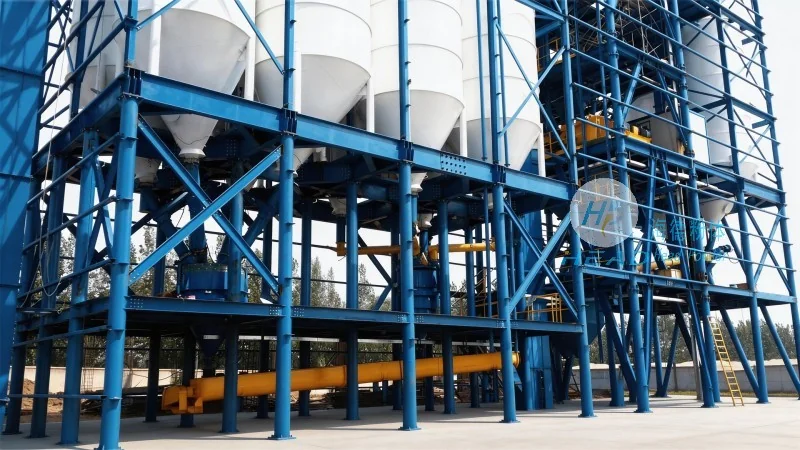
HeadPowder's Airflow Conveying Solutions: A Specialized Approach
Shandong HeadPowder Engineering Co., Ltd., a leading provider of advanced material handling technologies, specializes in developing and implementing customized airflow conveying systems tailored to the unique requirements of molybdenum oxide transport. With a focus on precision, durability, and safety, HeadPowder's solutions are designed to address the specific challenges associated with handling this high-value material. The company's expertise lies in the integration of state-of-the-art components, including high-efficiency blowers, specialized ductwork, and advanced control systems, all optimized for the consistent and safe movement of molybdenum oxide.
Key Advantages of Airflow Conveying for Molybdenum Oxide
Implementing an airflow conveying system for molybdenum oxide offers several distinct advantages over conventional methods. Firstly, it significantly reduces the risk of dust exposure and contamination, which is crucial for maintaining product purity and compliance with industrial safety standards. Secondly, the system's ability to handle fine powders without clogging or degradation ensures consistent material quality throughout the transport process. Additionally, the enclosed nature of airflow conveying minimizes environmental impact by containing dust within the system, reducing the need for extensive dust control measures. From a practical standpoint, these systems often provide greater flexibility in layout and integration with existing industrial setups, allowing for seamless incorporation into production lines.
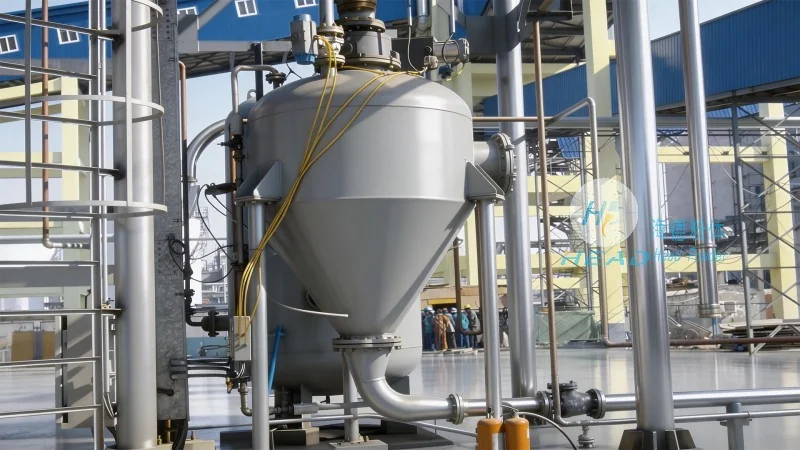
Customization and Scalability: Meeting Diverse Operational Needs
HeadPowder understands that each industrial facility has unique operational parameters and space constraints. Therefore, their airflow conveying solutions are highly customizable to meet specific requirements. Whether the application involves short-distance transport within a production facility or long-distance transfer between different processing units, the system can be scaled and configured accordingly. The company's engineering team works closely with clients to assess their current and future needs, designing systems that are not only efficient but also adaptable to potential expansions or changes in production volume. This approach ensures that the investment in an airflow conveying system provides long-term value and operational flexibility.
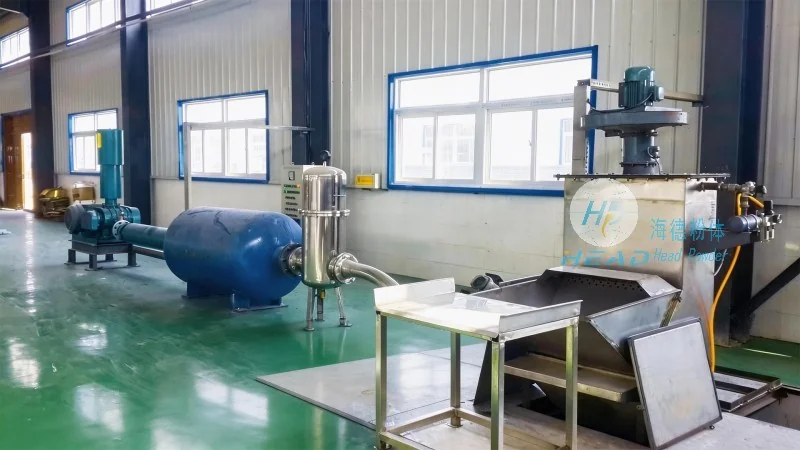
Reliability and Maintenance: Ensuring Continuous Operation
Reliability is a top priority in industrial material handling, and HeadPowder's airflow conveying systems are engineered for consistent performance. The use of high-quality components, such as robust blowers and durable ductwork, minimizes the risk of system failures and reduces the frequency of maintenance interventions. Additionally, the enclosed design of the system facilitates easier maintenance and cleaning, as dust and particles are contained within the system rather than spreading to the surrounding environment. This not only enhances operational efficiency but also reduces downtime associated with cleaning and maintenance tasks. By focusing on reliability and ease of maintenance, HeadPowder's solutions help clients maintain uninterrupted production processes, which is essential for meeting market demands and maintaining competitiveness.
Conclusion: A Proven Solution for Molybdenum Oxide Transport
In conclusion, the implementation of an efficient airflow conveying system by Shandong HeadPowder Engineering Co., Ltd. represents a significant advancement in the safe and effective handling of molybdenum oxide. By addressing the unique challenges associated with this material, the system provides a reliable, flexible, and cost-effective solution that enhances operational performance and safety. With a commitment to customization, reliability, and customer satisfaction, HeadPowder continues to be a trusted partner in the development of advanced material handling technologies for the molybdenum oxide industry. Based in Shandong, China, the company's expertise and innovative solutions have established it as a leader in providing tailored airflow conveying systems that meet the evolving needs of industrial applications.