

[Efficient Pneumatic Conveying Solutions for Cocoa Powder Handling Challenges]
When it comes to transporting cocoa powder, traditional methods often fall short in meeting the demands of modern production lines. The fine, dry nature of cocoa powder makes it susceptible to caking, dusting, and loss during handling. This is where advanced pneumatic conveying systems come into play, offering a reliable and efficient solution to overcome these common challenges. The systems utilize air pressure to move the powder through pipelines, ensuring a clean, controlled, and safe transfer process.
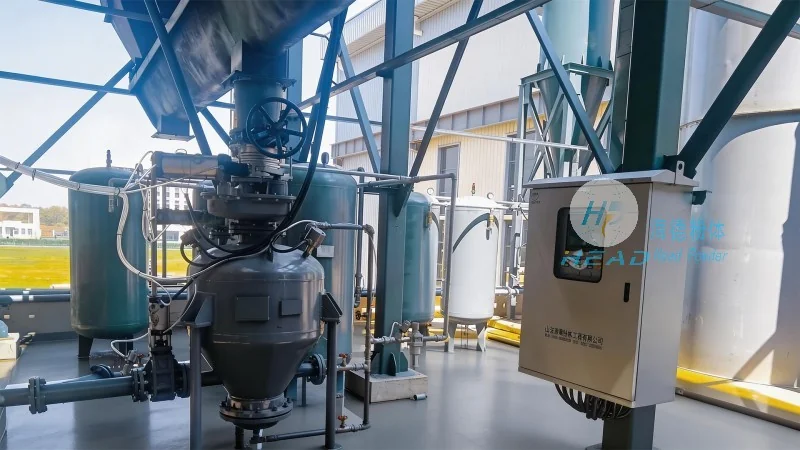
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading provider of specialized engineering solutions for powder handling and material transport. With a strong focus on innovation and customer-centric design, the company has established itself as a trusted partner in the food processing and industrial sectors. HeadPowder specializes in developing tailored pneumatic conveying systems that address the unique requirements of various powder materials, including cocoa powder. The company’s expertise lies in creating efficient, low-maintenance, and cost-effective solutions that enhance operational productivity while maintaining product quality.
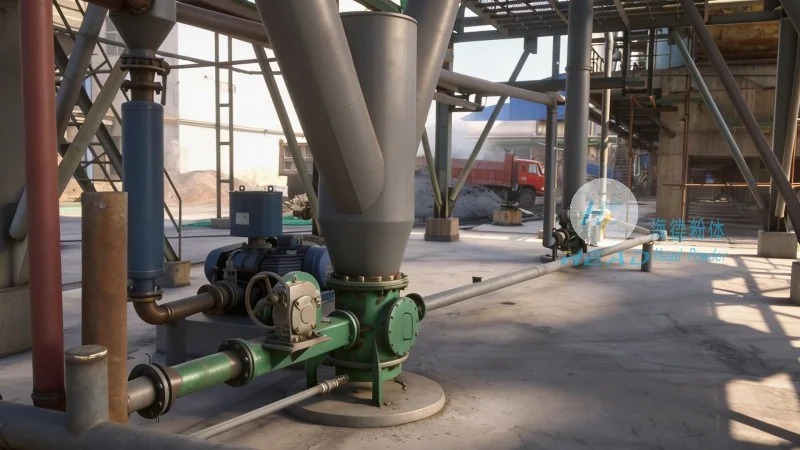
Key Features of Pneumatic Conveying Systems for Cocoa Powder
HeadPowder’s pneumatic conveying systems are engineered with several key features that make them ideal for cocoa powder handling. Firstly, the systems employ positive pressure or negative pressure conveying methods, depending on the specific application requirements. Positive pressure systems are commonly used for long-distance or high-capacity transport, where air is forced through the pipeline to move the powder. Negative pressure systems, on the other hand, are suitable for short-distance or low-volume applications, where air is drawn through the system to pull the powder. Both methods ensure minimal product degradation and prevent contamination. Additionally, the systems are equipped with advanced control mechanisms that allow for precise flow regulation, ensuring consistent and reliable transport. The use of stainless steel or food-grade materials in the construction of the pipelines and components further enhances hygiene and compliance with industry standards. This combination of features makes the systems highly effective in maintaining the quality and integrity of cocoa powder throughout the conveying process.
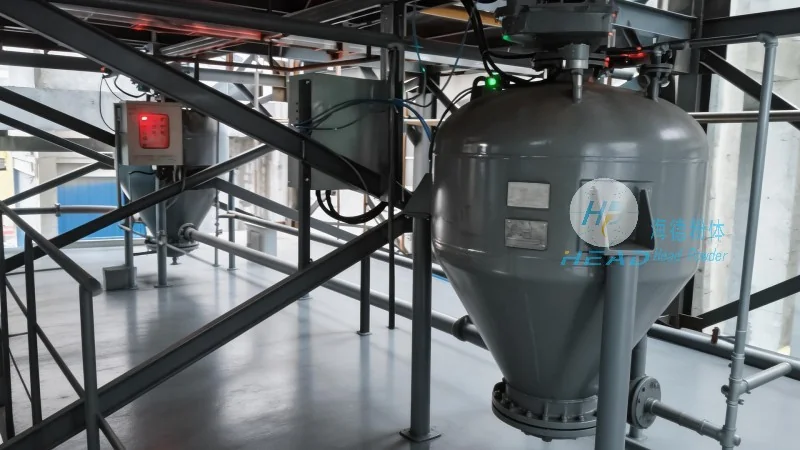
Benefits of Implementing Pneumatic Conveying for Cocoa Powder
Adopting pneumatic conveying systems for cocoa powder handling offers numerous benefits for businesses. One of the primary advantages is the significant reduction in product loss and contamination. Unlike traditional methods such as bucket elevators or belt conveyors, pneumatic systems minimize the risk of dust generation and product spillage, leading to higher material recovery rates. This not only improves efficiency but also reduces waste and associated costs. Another key benefit is the enhanced safety and hygiene. The enclosed pipeline system prevents exposure to airborne particles, protecting both the product and the operators from dust inhalation. This is particularly important in food processing environments where maintaining high standards of cleanliness is paramount. Furthermore, the systems offer flexibility in terms of layout and integration with existing production lines. They can be easily customized to fit various plant configurations, allowing for seamless integration without major modifications. The low maintenance requirements of these systems also contribute to long-term cost savings, as they require fewer parts and less frequent servicing compared to traditional conveyors.
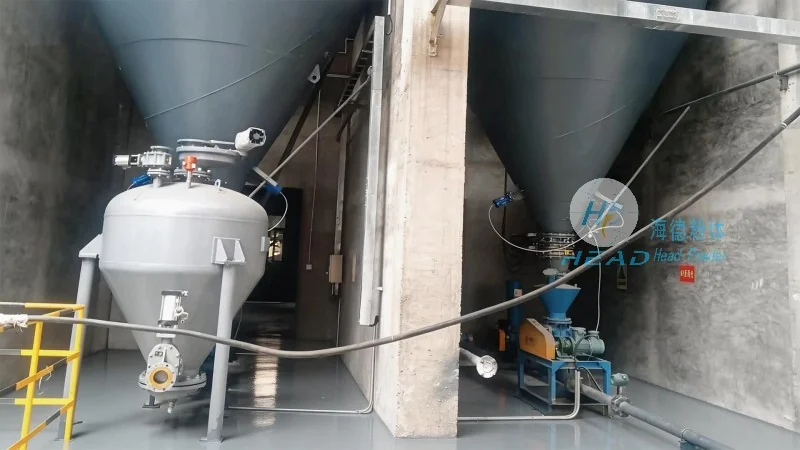
Tailored Solutions for Diverse Cocoa Powder Handling Needs
HeadPowder understands that each cocoa powder processing facility has unique operational needs. Therefore, the company provides customized pneumatic conveying solutions that are tailored to the specific requirements of each client. The engineering team at HeadPowder works closely with clients to assess their current processes, identify bottlenecks, and develop optimal conveying systems. This collaborative approach ensures that the final solution is not only efficient but also cost-effective and sustainable. The company’s expertise in material handling and process engineering allows for the design of systems that optimize energy consumption and reduce operational costs. By leveraging advanced technology and years of industry experience, HeadPowder delivers solutions that meet the highest standards of performance and reliability. Whether it’s for small-scale production or large industrial facilities, the company’s pneumatic conveying systems are designed to handle the demands of cocoa powder transport with precision and efficiency.