

[Efficient and Clean Stone Conveying: An In-Depth Look at Pneumatic Conveying Technology]
When it comes to transporting aggregates like stones and gravel, efficiency and cleanliness are paramount in industrial operations. Traditional methods such as belt conveyors or bucket elevators often face challenges like material spillage, contamination, and operational inefficiencies. This is where pneumatic conveying technology steps in as a superior solution. Pneumatic conveying systems utilize air to transport bulk materials, offering a clean, enclosed, and highly efficient method for moving stone and other aggregates. For companies in the construction and mining sectors, adopting such technology can significantly enhance productivity while maintaining a clean working environment.
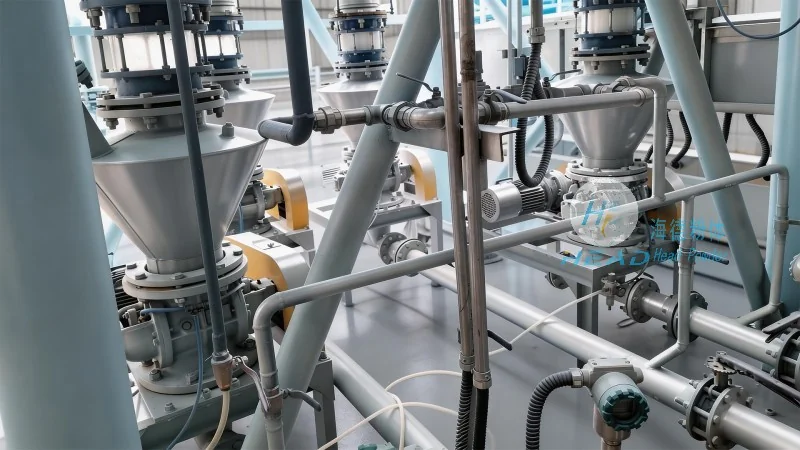
Pneumatic Conveying Technology: How It Works
Pneumatic conveying systems operate by using compressed air to create a flow that moves materials through a pipeline. There are two main types: pressure and vacuum systems. Pressure systems use positive pressure to push material through the line, while vacuum systems use negative pressure to pull material from a hopper or storage area. For stone handling, pressure systems are often preferred due to their ability to handle abrasive materials and maintain consistent flow rates. The process involves loading the stone into a hopper, which then feeds into the conveying line. The air flow ensures the material is transported smoothly without the need for manual handling or exposure to dust and debris.
Benefits of Pneumatic Conveying for Stone Transport
Implementing pneumatic conveying for stone transport offers numerous advantages. Firstly, it provides a completely enclosed system, preventing dust and particles from entering the workplace or the environment. This is crucial for maintaining air quality and compliance with environmental regulations. Secondly, the technology reduces material loss and spillage, as the system is fully contained. This not only saves on material costs but also minimizes cleanup efforts. Thirdly, pneumatic conveying systems can handle a wide range of stone sizes and types, from fine gravel to larger aggregates, without the need for additional processing. The consistent flow and low maintenance requirements also contribute to operational efficiency, making it a cost-effective solution in the long run.
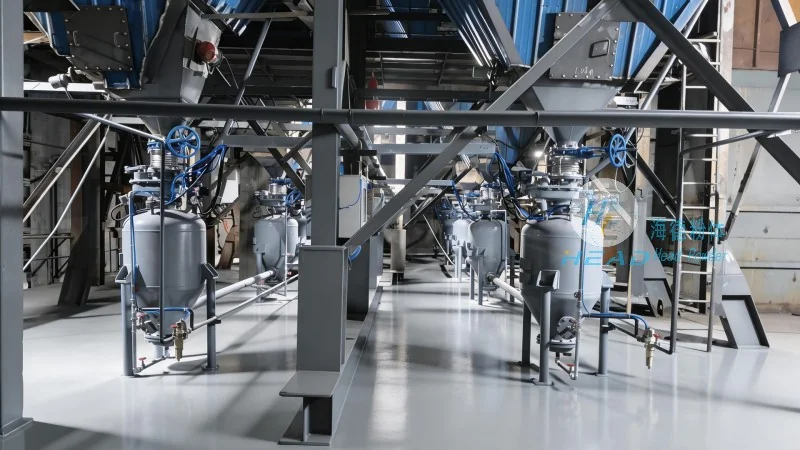
HeadPowder Engineering: Your Partner in Clean and Efficient Stone Conveying
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, specializes in designing and supplying advanced pneumatic conveying systems tailored to the needs of stone and aggregate industries. With years of experience and a commitment to quality, HeadPowder offers customized solutions that meet the specific requirements of each client. The company’s products are engineered to handle the toughest materials, ensuring durability and reliability in demanding environments. By choosing HeadPowder, businesses can enhance their stone handling processes, reduce operational costs, and achieve a cleaner, more efficient workflow.
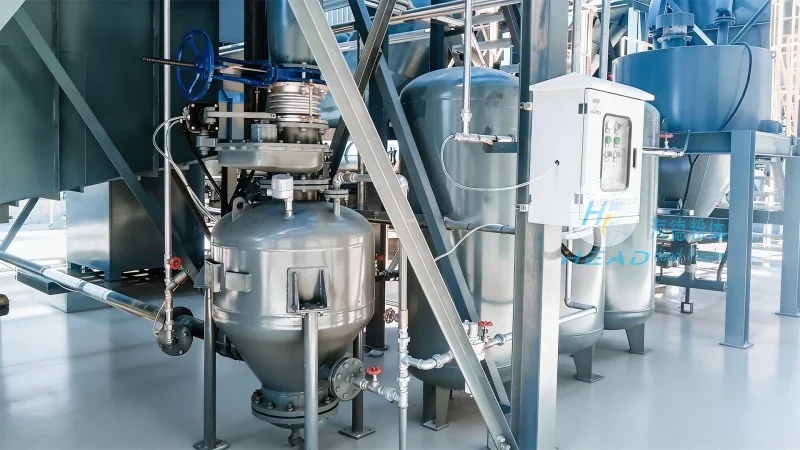
Key Features of HeadPowder’s Pneumatic Conveying Solutions
HeadPowder’s pneumatic conveying systems are equipped with several key features that set them apart in the market. These include robust material handling capabilities, suitable for both dry and wet stone applications. The systems are designed with high-quality components that resist wear and tear, ensuring long-term performance. Additionally, the company provides comprehensive after-sales support, including installation, maintenance, and technical assistance. This ensures that clients receive not just a product but a complete solution that meets their operational needs. The systems are also scalable, allowing businesses to expand their operations without the need for major overhauls.
Conclusion: The Future of Stone Conveying with Pneumatic Technology
As the construction and mining industries continue to evolve, the demand for efficient and clean material handling solutions grows. Pneumatic conveying technology, with its ability to deliver superior performance and environmental benefits, is becoming an increasingly popular choice. For companies looking to enhance their stone transport processes, partnering with a reputable manufacturer like Shandong HeadPowder Engineering Co., Ltd. is the first step towards achieving operational excellence. By investing in pneumatic conveying systems, businesses can improve productivity, reduce costs, and maintain a clean and safe working environment. The future of stone conveying lies in the integration of advanced technology and reliable engineering, and HeadPowder is at the forefront of this evolution.