

[Dust Pneumatic Conveying Systems: The Intelligent and Efficient New Era of Dust Transport]
Efficient and intelligent dust handling solutions are now more accessible than ever, thanks to advanced pneumatic conveying systems. These systems represent a significant advancement in material transport technology, offering a reliable and versatile method for moving dust and powders across various industrial applications.
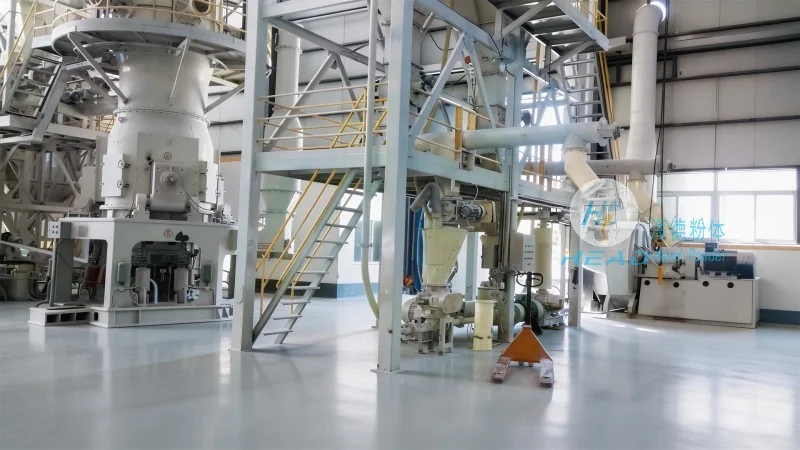
Pneumatic Conveying Systems: Core Technology and Benefits
The heart of dust pneumatic conveying lies in the use of compressed air to transport particulate materials. This technology eliminates the need for traditional mechanical components like belts or screws, reducing maintenance requirements and operational downtime. The system works by creating a pressure differential that draws the material through a pipeline, ensuring a smooth and continuous flow. Key benefits include improved safety by minimizing human contact with dust, enhanced hygiene in food and pharmaceutical industries, and the ability to handle a wide range of materials from fine powders to bulk solids.
HeadPowder Engineering: Expert in Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of customized pneumatic conveying systems. With a strong presence in China, particularly in Shandong, the company specializes in designing, manufacturing, and installing systems tailored to the specific needs of clients. HeadPowder’s expertise spans various industries, including chemical, food processing, and mining, where dust and powder handling are critical. The company’s commitment to quality and innovation ensures that each system is built to meet stringent industry standards and client expectations.
Customization and Versatility in Dust Pneumatic Conveying
One of the standout features of HeadPowder’s systems is their adaptability. Whether the application involves short-distance transport or long-distance pipelines, the company offers solutions that can be scaled to meet the requirements. The systems can be configured for both positive and negative pressure operations, allowing flexibility in handling different materials and process conditions. This versatility makes them suitable for a wide array of applications, from small-scale laboratory use to large-scale industrial production lines. Additionally, the systems are designed with ease of maintenance in mind, featuring accessible components and user-friendly controls that reduce operational complexity.
Reliability and Performance in Industrial Settings
Reliability is paramount in industrial operations, and HeadPowder’s pneumatic conveying systems are engineered to deliver consistent performance. The use of high-quality materials and robust construction ensures durability under heavy usage and harsh environmental conditions. The systems are equipped with advanced monitoring and control features, allowing real-time tracking of material flow and system performance. This not only enhances operational efficiency but also enables proactive maintenance, minimizing unexpected breakdowns and maximizing uptime. Clients benefit from reduced operational costs and increased productivity, as the systems require less energy and maintenance compared to traditional methods.
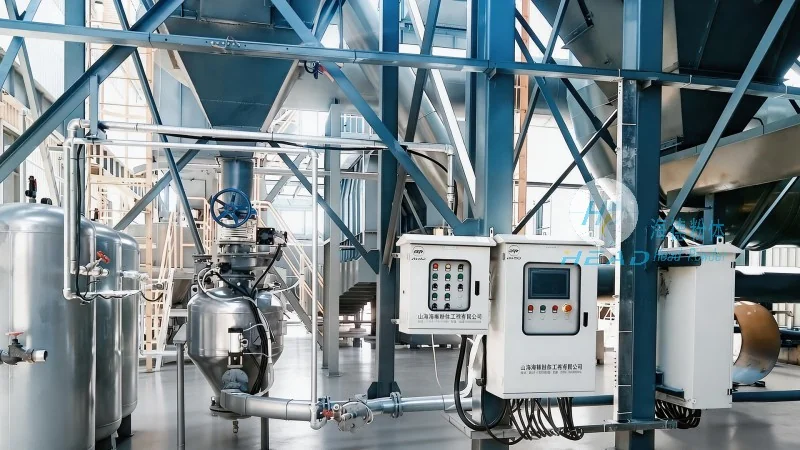
Application Examples and Industry Impact
HeadPowder’s dust pneumatic conveying systems have been successfully implemented in numerous industries, demonstrating their effectiveness in real-world scenarios. In the chemical industry, they are used to transport raw materials and finished products, ensuring a clean and efficient process. In food processing, the systems maintain high hygiene standards, preventing contamination and ensuring product quality. The mining sector also benefits from these systems, as they efficiently handle bulk materials like coal and ore, improving overall production efficiency. These applications highlight the versatility and reliability of HeadPowder’s solutions, making them a preferred choice for businesses seeking to optimize their dust handling processes.